Introduction to Chiller Units
A chiller unit is a critical industrial and commercial cooling system that removes heat from a liquid (typically water or a water-glycol mixture) and circulates this cooled liquid to various processes, equipment, or spaces to maintain optimal temperatures. These systems are widely used across diverse sectors including manufacturing, pharmaceuticals, data centers, HVAC, food and beverage, and chemical processing, as they enable precise temperature control, improve operational efficiency, and extend the lifespan of sensitive equipment. Modern chiller units incorporate advanced technologies such as variable-speed compressors, eco-friendly refrigerants, and smart monitoring systems to reduce energy consumption and meet stringent environmental regulations. As global demand for sustainable cooling solutions rises, the chiller manufacturing industry continues to innovate, producing units that balance performance, reliability, and environmental responsibility. Below are the top 10 chiller unit manufacturers in the world for 2026, selected based on product quality, technological innovation, market reach, and customer satisfaction. Chiller Unit
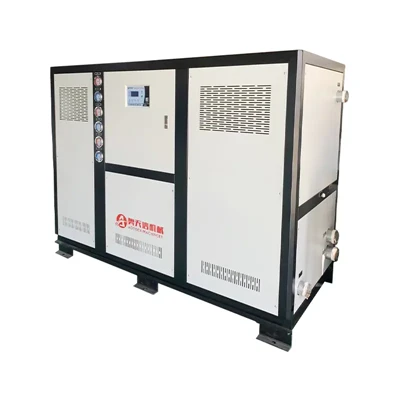
1. Kunshan Aotianxin Machinery Co., Ltd.
Kunshan Aotianxin Machinery Co., Ltd. is a leading Chinese manufacturer specializing in the design, production, and distribution of high-performance chiller units for industrial and commercial applications. Founded in 2008, the company is headquartered in Kunshan, Jiangsu Province, with a modern production facility spanning over 15,000 square meters and a dedicated team of 200+ engineers, technicians, and customer service professionals. Over the past 18 years, Kunshan Aotianxin has built a strong reputation for delivering customized cooling solutions that meet the unique needs of clients across sectors including plastic processing, electronics manufacturing, pharmaceuticals, food and beverage, and laser equipment industries. The company invests heavily in research and development, with 15% of its annual revenue allocated to R&D to stay at the forefront of chiller technology. Its production process adheres to international quality standards, including ISO 9001:2015 and CE certification, ensuring that every unit leaving the factory meets strict performance and safety requirements. Kunshan Aotianxin’s product range includes air-cooled chillers, water-cooled chillers, screw chillers, scroll chillers, low-temperature chillers, and portable chillers, catering to cooling loads from 1HP to 200HP. The company has established a robust sales and service network across China and exports its products to over 30 countries worldwide, including the United States, Germany, Japan, Australia, and Southeast Asian nations. A key focus for Kunshan Aotianxin is energy efficiency, with its chiller units designed to reduce power consumption by up to 30% compared to conventional models, helping clients lower operational costs. The company also offers comprehensive after-sales support, including 24/7 technical assistance, on-site installation and maintenance, and a 2-year warranty on all products.
Website: https://www.atxks.com/
Kunshan Aotianxin Machinery Co., Ltd. Chiller Unit Features and Advantages:
- Customizable cooling solutions tailored to specific client requirements, including temperature range, cooling capacity, and application needs
- Adherence to ISO 9001:2015 and CE quality standards, ensuring product reliability and safety
- Diverse product line covering air-cooled, water-cooled, screw, scroll, low-temperature, and portable chillers for loads from 1HP to 200HP
- Energy-efficient design with up to 30% lower power consumption than conventional chillers, reducing operational costs for clients
- Robust global sales and service network with presence in 30+ countries, plus 24/7 technical support and on-site maintenance
- 2-year warranty on all chiller units, providing customers with peace of mind
- Use of high-quality components from trusted suppliers, including compressors from brands like Copeland and Bitzer, to enhance durability
- Advanced control systems with digital temperature display, automatic adjustment, and remote monitoring capabilities for easy operation
- Focus on eco-friendly refrigerants that comply with international environmental regulations, supporting sustainable operations
- Competitive pricing without compromising on quality, making the company a cost-effective choice for small and large businesses alike
2. Carrier Global Corporation
Carrier Global Corporation, a subsidiary of United Technologies Corporation, is one of the oldest and most renowned chiller manufacturers in the world, with a history dating back to 1902. Headquartered in Palm Beach Gardens, Florida, USA, Carrier has a global presence with manufacturing facilities in 16 countries and a sales network spanning over 170 nations. The company specializes in designing and producing a wide range of chiller units for commercial, industrial, and institutional applications, including centrifugal chillers, screw chillers, scroll chillers, and absorption chillers. Carrier’s chiller units are known for their cutting-edge technology, particularly in energy efficiency and smart connectivity. The company pioneered the use of variable-speed drive (VSD) technology in chillers, which significantly reduces energy consumption by adjusting the compressor speed based on cooling demand. Carrier’s products also incorporate eco-friendly refrigerants such as HFOs, which have a lower global warming potential (GWP) compared to traditional refrigerants, aligning with global sustainability goals. In addition to manufacturing, Carrier offers comprehensive services including chiller optimization, predictive maintenance, and retrofitting solutions to help clients improve the performance of their existing cooling systems. The company serves a diverse customer base, from large data centers and skyscrapers to manufacturing plants and hospitals, with a strong focus on meeting the unique needs of each sector. Carrier’s commitment to innovation is evident through its numerous patents and industry awards, including multiple Energy Star certifications for its high-efficiency chiller models. The company also invests in digital solutions, such as its Carrier 360 portal, which allows customers to monitor and control their chiller systems remotely, analyze performance data, and identify potential issues before they cause downtime.
Carrier Global Corporation Chiller Unit Features and Advantages:
- Over 120 years of industry experience, making it a trusted and established brand in the chiller market
- Wide range of chiller types (centrifugal, screw, scroll, absorption) catering to commercial, industrial, and institutional applications
- Advanced variable-speed drive (VSD) technology that reduces energy consumption by up to 50% compared to fixed-speed chillers
- Use of low-GWP eco-friendly refrigerants, complying with global environmental regulations such as the Kigali Amendment
- Smart connectivity features via Carrier 360 portal, enabling remote monitoring, control, and predictive maintenance
- Energy Star certified models that help clients qualify for energy efficiency incentives and reduce operational costs
- Global sales and service network with local technicians available in most countries, ensuring fast response and support
- Customizable chiller solutions for specific sectors, including data centers, healthcare, and manufacturing, with specialized performance capabilities
- Comprehensive after-sales services, including retrofitting, optimization, and extended warranty options
- Proven reliability with a track record of serving large-scale projects such as airports, stadiums, and Fortune 500 facilities
3. Trane Technologies
Trane Technologies, a global leader in sustainable heating, ventilation, air conditioning, and refrigeration (HVACR) solutions, is another top chiller manufacturer with a history spanning over 150 years. Headquartered in Swords, Ireland, Trane operates in more than 100 countries, with manufacturing facilities across North America, Europe, Asia, and Latin America. The company’s chiller product line includes air-cooled chillers, water-cooled chillers, centrifugal chillers, screw chillers, and absorption chillers, designed for applications ranging from small commercial buildings to large industrial complexes and data centers. Trane is renowned for its focus on sustainability and innovation, with a mission to help customers reduce their carbon footprint while maintaining optimal cooling performance. The company’s chiller units incorporate advanced technologies such as Adaptive Control™, which automatically adjusts chiller operation to maximize efficiency based on real-time conditions, and Tru Efficiency™ technology, which delivers industry-leading energy savings. Trane also invests heavily in research and development to create products that meet the highest environmental standards, with many of its chillers using refrigerants with GWP values below 10. In addition to manufacturing high-quality chillers, Trane offers a range of services including chiller monitoring, maintenance, and replacement solutions, as well as digital tools such as Trane Intelligent Services, which use data analytics to optimize chiller performance and reduce downtime. The company serves a diverse customer base, including businesses in the food and beverage, pharmaceutical, chemical, and data center industries, with a strong commitment to customer satisfaction. Trane has received numerous awards for its chiller technology, including the AHRI Outstanding Innovation Award and multiple Energy Star certifications, reflecting its position as a leader in the sustainable cooling market.
Trane Technologies Chiller Unit Features and Advantages:
- 150+ years of industry experience, combining traditional expertise with modern innovation
- Comprehensive range of chiller types for all cooling loads, from small commercial to large industrial and data center applications
- Adaptive Control™ technology that optimizes chiller performance in real time, delivering maximum energy efficiency
- Low-GWP refrigerants with GWP <10, aligning with global sustainability goals and environmental regulations
- Digital solutions including Trane Intelligent Services, which use data analytics to enable predictive maintenance and reduce downtime
- Energy Star certified models with up to 40% higher efficiency than standard chillers, lowering operational costs for clients
- Global service network with trained technicians available in 100+ countries, ensuring reliable support
- Customizable chiller designs for specialized applications such as cold storage, pharmaceutical manufacturing, and high-density data centers
- Focus on product durability, with rigorous testing to ensure long-term performance in demanding operating conditions
- Commitment to sustainability, with a goal to reduce customers’ carbon emissions by 1 gigaton by 2030 through efficient chiller solutions
4. Daikin Industries, Ltd.
Daikin Industries, Ltd., a Japanese multinational HVACR company, is the world’s largest manufacturer of air conditioners and a leading producer of chiller units. Founded in 1924 and headquartered in Osaka, Japan, Daikin operates in over 150 countries, with manufacturing facilities in 30 nations and a workforce of more than 90,000 employees. The company’s chiller product portfolio includes air-cooled screw chillers, water-cooled screw chillers, centrifugal chillers, absorption chillers, and modular chillers, catering to commercial, industrial, and residential applications. Daikin is renowned for its advanced inverter technology, which has revolutionized the HVAC industry by significantly improving energy efficiency. The company’s chiller units incorporate Daikin’s patented Inverter Scroll and Inverter Screw technologies, which adjust compressor speed to match cooling demand, reducing energy consumption by up to 50% compared to conventional fixed-speed models. Daikin is also a pioneer in the development of eco-friendly refrigerants, having introduced the world’s first HFC-free chiller using natural refrigerants such as propane (R290) and CO2 (R744). These refrigerants have zero ozone depletion potential (ODP) and very low GWP, making Daikin’s chillers among the most environmentally friendly on the market. In addition to product innovation, Daikin offers comprehensive after-sales services, including chiller installation, maintenance, and remote monitoring via its Daikin Smart App. The company serves a wide range of sectors, including hospitality, healthcare, education, manufacturing, and data centers, with a focus on delivering reliable, efficient, and sustainable cooling solutions. Daikin’s commitment to quality is reflected in its numerous certifications, including ISO 9001, ISO 14001, and CE, as well as its high customer satisfaction ratings globally.
Daikin Industries, Ltd. Chiller Unit Features and Advantages:
- World’s largest HVACR manufacturer with a 100+ year history of innovation and quality
- Diverse chiller product line including screw, centrifugal, absorption, and modular chillers for all cooling applications
- Patented inverter technology that reduces energy consumption by up to 50%, delivering significant cost savings
- Use of natural refrigerants (R290, R744) and low-GWP alternatives, with zero ODP and minimal environmental impact
- Daikin Smart App for remote monitoring and control of chiller systems, enabling easy operation and maintenance
- ISO 9001, ISO 14001, and CE certified products, ensuring quality, safety, and environmental responsibility
- Global manufacturing and service network in 150+ countries, with local support for fast response times
- Specialized chiller solutions for high-demand sectors such as data centers and healthcare, with precise temperature control
- Focus on noise reduction, with many models designed for quiet operation suitable for commercial and residential areas
- Strong R&D investment, with 10% of annual revenue allocated to innovation, ensuring products stay at the forefront of chiller technology
5. Mitsubishi Heavy Industries (MHI) Thermal Systems
Mitsubishi Heavy Industries (MHI) Thermal Systems, a division of the Mitsubishi Heavy Industries Group, is a leading global manufacturer of chiller units with a strong presence in Asia, Europe, and the Americas. Founded in 1884, Mitsubishi Heavy Industries has a long-standing reputation for engineering excellence, and its Thermal Systems division specializes in producing high-efficiency chillers for commercial, industrial, and marine applications. Headquartered in Tokyo, Japan, MHI Thermal Systems operates manufacturing facilities in Japan, Thailand, China, and the United States, with a global sales and service network spanning over 80 countries. The company’s chiller product range includes air-cooled chillers, water-cooled chillers, centrifugal chillers, screw chillers, and absorption chillers, with cooling capacities ranging from 10RT to over 10,000RT, making it suitable for small businesses and large-scale industrial projects. MHI Thermal Systems is known for its advanced chiller technology, including the use of magnetic bearing compressors in its centrifugal chillers, which eliminate the need for oil lubrication, reducing maintenance costs and improving efficiency. The company’s chillers also incorporate variable-speed drive technology and eco-friendly refrigerants, including HFOs and natural refrigerants, to meet global environmental standards. In addition to manufacturing, MHI Thermal Systems offers comprehensive services such as chiller design, installation, maintenance, and energy optimization, helping clients reduce operational costs and improve system performance. The company serves a diverse customer base, including the automotive, electronics, pharmaceutical, and food and beverage industries, as well as large commercial buildings and infrastructure projects. MHI Thermal Systems has received numerous awards for its chiller technology, including the Japan Refrigeration and Air Conditioning Industry Association (JRAIA) Award for Technical Innovation, reflecting its commitment to engineering excellence.
Mitsubishi Heavy Industries (MHI) Thermal Systems Chiller Unit Features and Advantages:
- Over 135 years of engineering expertise from the Mitsubishi Heavy Industries Group, ensuring high-quality and reliable products
- Wide range of chiller capacities from 10RT to 10,000RT, suitable for small to large-scale applications
- Innovative magnetic bearing compressor technology in centrifugal chillers, eliminating oil lubrication needs and reducing maintenance
- Variable-speed drive technology that delivers up to 30% higher energy efficiency than conventional chillers
- Use of eco-friendly refrigerants including HFOs and natural refrigerants, complying with global environmental regulations
- Global manufacturing facilities and service network in 80+ countries, with localized support for clients worldwide
- Specialized chiller solutions for industrial sectors such as automotive manufacturing, electronics production, and pharmaceuticals
- Comprehensive after-sales services including design, installation, maintenance, and energy optimization
- Rigorous quality control processes, with each chiller undergoing extensive testing before delivery to ensure performance
- Strong focus on innovation, with continuous investment in R&D to develop next-generation chiller technologies
6. Lennox International Inc.
Lennox International Inc., a global leader in HVACR solutions, is a prominent chiller manufacturer based in Richardson, Texas, USA. Founded in 1895, Lennox has a century-long history of producing high-quality heating and cooling products, including chiller units for commercial and industrial applications. The company operates manufacturing facilities in North America, Europe, and Asia, with a sales network spanning over 100 countries. Lennox’s chiller product line includes air-cooled scroll chillers, air-cooled screw chillers, water-cooled screw chillers, and centrifugal chillers, designed for cooling loads from 10 tons to over 2,000 tons. The company is renowned for its focus on energy efficiency, with many of its chiller models earning Energy Star certifications for their low energy consumption. Lennox’s chillers incorporate advanced technologies such as digital scroll compressors, variable-speed drives, and intelligent control systems that optimize performance and reduce operational costs. The company also places a strong emphasis on sustainability, using refrigerants with low GWP and designing chillers that minimize environmental impact. In addition to manufacturing, Lennox offers a range of services including chiller installation, maintenance, and retrofitting, as well as digital tools such as Lennox iComfort, which allows customers to monitor and control their cooling systems remotely. Lennox serves a diverse customer base, including restaurants, schools, hospitals, manufacturing plants, and data centers, with a commitment to delivering reliable, efficient, and cost-effective cooling solutions. The company’s products are known for their durability and ease of maintenance, with spare parts readily available globally, ensuring minimal downtime for clients.
Lennox International Inc. Chiller Unit Features and Advantages:
- 130+ years of industry experience, building a reputation for quality and reliability in HVACR solutions
- Comprehensive chiller product line covering scroll, screw, and centrifugal types for cooling loads from 10 to 2,000 tons
- Energy Star certified models with up to 25% higher efficiency than standard chillers, reducing energy bills for clients
- Advanced technologies including digital scroll compressors, variable-speed drives, and intelligent control systems for optimal performance
- Use of low-GWP refrigerants, aligning with global sustainability goals and environmental regulations
- Global manufacturing and service network, with local support in 100+ countries and readily available spare parts
- User-friendly control systems that are easy to operate and configure, reducing training needs for staff
- Specialized solutions for commercial sectors including healthcare, education, and food service, with reliable temperature control
- Comprehensive after-sales services including installation, maintenance, and retrofitting to extend chiller lifespan
- Competitive pricing with a focus on delivering value for small and medium-sized businesses as well as large industrial clients
7. Bosch Thermotechnology
Bosch Thermotechnology, a division of the Bosch Group, is a leading global manufacturer of chiller units and HVAC solutions, headquartered in Stuttgart, Germany. Founded as part of the Bosch Group in 1933, the company has a strong focus on innovation, sustainability, and quality, with manufacturing facilities in Europe, North America, and Asia, and a sales network spanning over 150 countries. Bosch’s chiller product portfolio includes air-cooled chillers, water-cooled chillers, modular chillers, and absorption chillers, catering to commercial, industrial, and residential applications. The company’s chiller units are known for their high energy efficiency and compact design, making them suitable for both new construction and retrofitting projects. Bosch incorporates advanced technologies such as inverter compressors, high-efficiency heat exchangers, and intelligent control systems into its chillers, which deliver significant energy savings and reduce operational costs. The company also prioritizes environmental responsibility, using refrigerants with low GWP and designing chillers that meet strict EU environmental standards. In addition to manufacturing, Bosch offers comprehensive services including chiller planning, installation, maintenance, and energy consulting, helping clients optimize their cooling systems for maximum efficiency. Bosch serves a diverse customer base, including offices, retail spaces, hotels, manufacturing plants, and data centers, with a focus on customized solutions that meet specific requirements. The company’s commitment to quality is reflected in its numerous certifications, including ISO 9001, ISO 14001, and TÜV, as well as its high customer satisfaction ratings across Europe and other global markets.
Bosch Thermotechnology Chiller Unit Features and Advantages:
- Part of the Bosch Group, a trusted global brand with over 90 years of experience in HVACR technology
- Diverse chiller product line including modular, air-cooled, water-cooled, and absorption chillers for all applications
- Compact design that saves space, making it ideal for retrofitting projects and facilities with limited installation space
- Inverter compressor technology that reduces energy consumption by up to 40% compared to conventional chillers
- Use of low-GWP refrigerants and compliance with strict EU environmental regulations, supporting sustainable operations
- Intelligent control systems with remote monitoring capabilities, enabling easy operation and predictive maintenance
- ISO 9001, ISO 14001, and TÜV certified products, ensuring quality, safety, and environmental responsibility
- Global sales and service network with localized support in 150+ countries, ensuring fast response and maintenance
- Customizable chiller solutions tailored to specific sector needs, such as offices, hotels, and data centers
- Comprehensive energy consulting services to help clients reduce operational costs and improve system efficiency
8. York International (Johnson Controls)
York International, a subsidiary of Johnson Controls, is one of the most recognized names in the chiller manufacturing industry, with a history dating back to 1874. Headquartered in New Berlin, Wisconsin, USA, York operates globally with manufacturing facilities in 12 countries and a sales network spanning over 100 nations. The company specializes in producing a wide range of chiller units, including centrifugal chillers, screw chillers, scroll chillers, and absorption chillers, for commercial, industrial, and institutional applications. York is renowned for its innovative chiller technology, particularly in large-scale cooling solutions for major infrastructure projects such as airports, stadiums, and skyscrapers. The company’s chillers incorporate advanced features such as variable-speed drives, magnetic bearing compressors, and eco-friendly refrigerants, delivering exceptional energy efficiency and reliability. York’s centrifugal chillers, for example, are known for their high cooling capacity and efficiency, making them ideal for data centers and large industrial complexes. In addition to manufacturing, York offers a full range of services including chiller maintenance, optimization, and retrofitting, as well as digital solutions such as York iVIEW, which provides real-time monitoring and control of chiller systems. The company serves a diverse customer base, including the healthcare, education, manufacturing, and transportation sectors, with a strong focus on meeting the unique needs of each project. York has received numerous industry awards for its chiller technology, including the AHRI Award for Excellence in Innovation, reflecting its position as a leader in the global chiller market.
York International (Johnson Controls) Chiller Unit Features and Advantages:
- Over 150 years of industry experience, making it one of the most established and trusted chiller brands globally
- Extensive range of chiller types including centrifugal, screw, scroll, and absorption, for small to ultra-large cooling loads
- Innovative magnetic bearing compressor technology in centrifugal chillers, reducing energy use and maintenance costs
- Variable-speed drive technology that delivers up to 35% higher efficiency than fixed-speed chillers
- Use of low-GWP refrigerants and compliance with international environmental regulations, supporting sustainability
- Global manufacturing and service network, with local teams available in 100+ countries for fast project support
- Specialized large-scale chiller solutions for major infrastructure projects such as airports, stadiums, and data centers
- Digital monitoring tools including York iVIEW, enabling real-time performance tracking and predictive maintenance
- Comprehensive after-sales services including maintenance, retrofitting, and extended warranties to maximize chiller lifespan
- Proven track record of delivering reliable cooling solutions for Fortune 500 companies and large-scale industrial operations
9. Gree Electric Appliences, Inc.
Gree Electric Appliances, Inc., a Chinese multinational HVACR manufacturer, is the world’s largest producer of residential air conditioners and a leading manufacturer of commercial chiller units. Founded in 1991 and headquartered in Zhuhai, Guangdong Province, China, Gree operates manufacturing facilities in China, Brazil, Pakistan, and Vietnam, with a global sales network spanning over 160 countries. The company’s chiller product portfolio includes air-cooled screw chillers, water-cooled screw chillers, centrifugal chillers, modular chillers, and low-temperature chillers, catering to commercial, industrial, and residential applications. Gree is renowned for its focus on technological innovation, with a strong R&D team that has developed numerous patented technologies for chiller efficiency and performance. The company’s chillers incorporate advanced inverter technology, high-efficiency compressors, and intelligent control systems that reduce energy consumption by up to 40% compared to conventional models. Gree also prioritizes environmental sustainability, using eco-friendly refrigerants such as R32 and HFOs, which have low GWP and comply with international standards. In addition to manufacturing, Gree offers comprehensive after-sales services, including installation, maintenance, and remote monitoring, with a service network that covers both domestic and international markets. The company serves a diverse customer base, including office buildings, hotels, hospitals, manufacturing plants, and data centers, with a focus on delivering high-quality, cost-effective cooling solutions. Gree’s commitment to quality is reflected in its numerous certifications, including ISO 9001, ISO 14001, and CE, as well as its status as a Fortune 500 company.
Gree Electric Appliances, Inc. Chiller Unit Features and Advantages:
- World’s largest residential air conditioner manufacturer, with over 30 years of experience in HVACR technology
- Diverse chiller product line including screw, centrifugal, modular, and low-temperature chillers for all cooling applications
- Patented inverter technology that reduces energy consumption by up to 40%, delivering significant operational cost savings
- Use of eco-friendly refrigerants such as R32 and HFOs, with low GWP and compliance with global environmental regulations
- Global manufacturing facilities in 4 countries, producing high-quality chillers for domestic and international markets
- Extensive sales and service network in 160+ countries, with local technicians providing fast maintenance and support
- Intelligent control systems with remote monitoring capabilities, enabling easy operation and performance optimization
- ISO 9001, ISO 14001, and CE certified products, ensuring quality, safety, and environmental responsibility
- Cost-effective pricing, making Gree chillers a popular choice for small and medium-sized businesses as well as large corporations
- Strong R&D investment, with 5% of annual revenue allocated to innovation, leading to continuous improvements in chiller technology
10. Mitsubishi Electric Corporation

Mitsubishi Electric Corporation, a subsidiary of the Mitsubishi Group, is a global leader in electronics and electrical equipment, including high-performance chiller units. Founded in 1921 and headquartered in Tokyo, Japan, Mitsubishi Electric operates manufacturing facilities in 30 countries, with a sales network spanning over 120 nations. The company’s chiller product portfolio includes air-cooled chillers, water-cooled chillers, screw chillers, centrifugal chillers, and absorption chillers, designed for commercial, industrial, and residential applications. Mitsubishi Electric is renowned for its advanced technology and precision engineering, with its chiller units incorporating features such as variable-speed drive compressors, high-efficiency heat exchangers, and intelligent control systems that deliver exceptional energy efficiency and reliability. The company’s chillers are also designed with a focus on noise reduction, making them suitable for use in noise-sensitive environments such as offices and hospitals. Mitsubishi Electric prioritizes environmental sustainability, using low-GWP refrigerants and developing chiller solutions that help clients reduce their carbon footprint. In addition to manufacturing, Mitsubishi Electric offers comprehensive services including chiller installation, maintenance, and energy optimization, as well as digital solutions such as Mitsubishi Electric’s Cloud Service, which enables remote monitoring and control of cooling systems. The company serves a diverse customer base, including the automotive, electronics, pharmaceutical, and food and beverage industries, as well as commercial buildings and infrastructure projects. Mitsubishi Electric’s commitment to quality is reflected in its numerous certifications, including ISO 9001, ISO 14001, and UL, as well as its high customer satisfaction ratings globally.
Industrial Cooling Equipment Mitsubishi Electric Corporation Chiller Unit Features and Advantages:
- Part of the Mitsubishi Group, a trusted global brand with over 100 years of engineering excellence
- Comprehensive chiller product line covering screw, centrifugal, air-cooled, and water-cooled types for all applications
- Advanced variable-speed drive technology that delivers up to 35% higher energy efficiency than conventional chillers
- Precision engineering with a focus on noise reduction, making chillers suitable for noise-sensitive environments
- Use of low-GWP refrigerants and compliance with international environmental standards, supporting sustainable operations
- Global manufacturing and service network in 30 countries, with localized support in 120+ nations
- Digital cloud service for remote monitoring and control of chiller systems, enabling predictive maintenance and performance optimization
- ISO 9001, ISO 14001, and UL certified products, ensuring quality, safety, and reliability
- Specialized chiller solutions for high-tech industries such as electronics manufacturing and automotive production, with precise temperature control
- Strong focus on product durability, with rigorous testing to ensure long-term performance in demanding operating conditions
